About Alpha Blue 15-0 - 15-1 - 15-2 For Water Based Ink
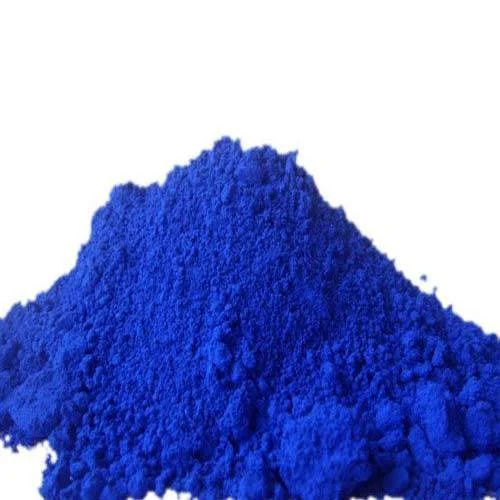
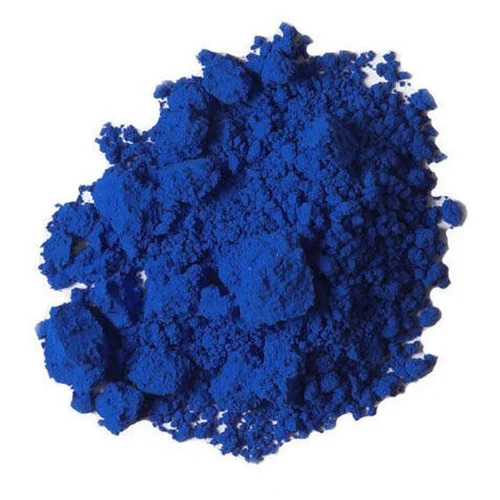
Take advantage of our best-seller, Alpha Blue 15-0 - 15-1 - 15-2, a commanding pigment designed to spotlight your water-based ink formulations. Decorated with superior features-bright blue shade, excellent light fastness (7-8), and remarkable heat stability (up to 250C)-this non-toxic, microfine powder is the preferred choice for printing, coatings, plastics, and textile applications. Its superior dispersibility, high purity (99%), and compatibility with most aqueous systems ensure outstanding performance. Packed in convenient 25 kg bags, Alpha Blue is your key to premium results. Elevate your ink production with this industrial-grade pigment-trusted across India and beyond.
Powerful & Versatile Usage Across Industries
Alpha Blue 15-0 - 15-1 - 15-2 for Water Based Ink is engineered as an industrial-grade, microfine organic pigment powder. It is ideal for diverse plant applications, including the manufacturing of printing inks, coatings, and textiles. Designed for easy application-simply mix with a suitable binder for water-based ink systems-its superior dispersibility and compatibility promise consistent, vibrant results in every usage, from large-scale production lines to smaller manufacturing facilities.
Market Value & Global Export Excellence
Experience impressive market value with Alpha Blue 15-0 - 15-1 - 15-2, a favored product in both domestic and international markets. Backed by express shipping and flexible payment terms, this pigment's demand is steadily growing across the globe. Major export estimates target Asia, Europe, and other key markets, while the main domestic market remains robust throughout India. Its reputation for reliability and superior performance ensures enduring customer satisfaction worldwide.
FAQ's of Alpha Blue 15-0 - 15-1 - 15-2 For Water Based Ink:
Q: How is Alpha Blue 15-0 - 15-1 - 15-2 applied in water-based ink systems?
A: Alpha Blue should be mixed with a binder in a water-based ink formulation, ensuring even dispersion for optimal color brightness and consistency in printing applications.
Q: What are the main benefits of using Alpha Blue for industrial applications?
A: This pigment offers bright blue color, high heat stability (up to 250C), excellent light fastness, and outstanding dispersibility, making it ideal for inks, coatings, plastics, and textiles.
Q: Where can Alpha Blue 15-0 - 15-1 - 15-2 be used?
A: It can be used in printing ink, paint, pigment production, plastic coloring, and textile printing processes across various industries.
Q: What is the recommended storage condition for this pigment?
A: Store Alpha Blue in a cool, dry place, away from sunlight and moisture, to maintain its quality and extend its shelf life up to 24 months.
Q: How does Alpha Blue ensure safety in usage?
A: Alpha Blue is formulated to be non-toxic and free of harmful substances, ensuring safe handling and application in various industrial and manufacturing environments.




 Send Inquiry


 Send Inquiry
